
Cable Tray Roll Forming Machines: Types and Applications
writer:fdcf9e6 release time:2026-11-19 18:24:04 Views:118frequency
Cable trays are the structural support systems that organize and protect power cables, data cables, and communication lines in commercial buildings, industrial plants, data centers, and major infrastructure. Instead of pulling every wire through conduit, cables are laid openly in a tray, which is cheaper, more ventilated, and far easier to modify. Cable tray roll forming machines produce these components in a continuous, automated process. This guide explains the different tray types, the standards and load classes that govern them, how punching and forming work, the accessories needed for a complete system, and the growing demand driven by data center and renewable energy construction.
1. What Is a Cable Tray?
A cable tray is a rigid unit or assembly of units, consisting of a base and side rails, that supports insulated cables. It is part of the cable management system, used wherever cables need to be routed across a building or plant. Trays are an alternative to conduit and trunking: they are open or partially open, so cables are accessible for inspection, maintenance, and future additions, and airflow around the cables helps dissipate heat, which allows higher cable ratings.
Trays are typically made from galvanized steel, stainless steel, or aluminum, chosen for the environment. Thickness ranges from about 1.0mm to 2.5mm depending on tray width and load. They are produced as straight sections on a roll forming line, then combined with fittings on site to build the complete route. Because trays are installed in long runs and repeated across every floor, they are a high-volume, repeatable product well suited to roll forming.
2. Main Cable Tray Types
2.1 Solid Bottom Tray
A solid bottom tray has a flat, unperforated base with side rails, giving cables the most physical protection and shielding them from dust and debris. It is used in clean environments, where small cables could fall through openings, or where EMI shielding and a degree of fire containment are wanted. Solid bottom trays are often fitted with covers. They are formed by creating the flat base and folding up the side rails, without a punching station.
2.2 Perforated Tray
Perforated trays have holes or slots in the base and sometimes the rails, balancing protection with ventilation and convenient cable tying. They are the most common general-purpose tray, used in commercial buildings and industrial plants. The holes are punched in the flat sheet before forming, using a die with a regular hole pattern. Ventilation keeps cables cooler and reduces the buildup of heat and moisture, while the solid webs still support cables continuously.
2.3 Ladder Tray
A ladder tray consists of two side rails connected by horizontal rungs at regular intervals, like a ladder. It is open, strong, and highly ventilated, designed for heavy power cables and large cable volumes in industrial and utility applications. Cables are easily pulled and accessed, and the rungs provide natural tie points. Ladder tray lines are more complex because they form the side rails and must incorporate or assemble the rungs, often in a separate operation.
2.4 Channel and Wire Mesh Tray
Channel trays are small, shallow U-shaped sections for light-duty cable runs and instrumentation. Wire mesh or basket trays are welded wire grids for light data and office cabling. These handle smaller cable loads and are common in ceiling voids and office fit-outs. Channel trays are simple to roll form, while wire mesh is usually produced by welding rather than roll forming.
3. Tray Type Comparison
| Type | Ventilation | Load | Main Application |
|---|---|---|---|
| Solid bottom | Low | Medium | Clean rooms, protected runs |
| Perforated | Medium | Medium-High | General commercial, industrial |
| Ladder | High | High | Heavy power, utility, industrial |
| Channel | Low | Low | Small cables, instrumentation |
4. Standards and Load Classes
4.1 Key Standards
Metal cable trays are governed by standards such as NEMA VE 1 in North America and IEC 61537 internationally, which define dimensions, load ratings, test methods, and finishing requirements. These standards ensure trays from different manufacturers are comparable and that published load capacities are based on consistent testing. Project specifications also reference electrical codes covering installation, bonding, and support spacing.
4.2 Load Classes and Span Ratings
Trays are rated by their safe working load over a specified support span, expressed in kilograms per meter or pounds per foot. The load class is verified by a deflection test, with limits such as span/200. A tray's published capacity always goes together with its support spacing — the same section supports more load over shorter spans. Engineers select the tray width, rail depth, and material thickness from the load tables to carry the actual cable weight plus any future additions and a safety margin.
| NEMA Load Class | Typical Load (lb/ft) | Typical Use |
|---|---|---|
| 50 | Light data, small cables | |
| 8A / 8B | 80 | General commercial |
| 12A / 12B | 120 | Industrial power cables |
| 20A / 20C | 200 | Heavy utility, long spans |
5. Materials and Finishes
5.1 Galvanized Steel
Hot-dip galvanized steel is the standard for general and outdoor use, providing a thick zinc coating that resists corrosion. Pre-galvanized coil is cheaper but has a lighter coating and cut edges that may need touch-up. For severe environments, stainless steel (304 or 316) or aluminum is used, with aluminum also offering light weight and natural corrosion resistance.
5.2 Special Coatings
Epoxy, polyester powder, or special paint finishes are applied for chemical environments, clean rooms, or aesthetic requirements. The finish must be specified together with the service environment, because corrosion is the main long-term failure mode. Material certificates and coating thickness checks support quality assurance on critical projects.
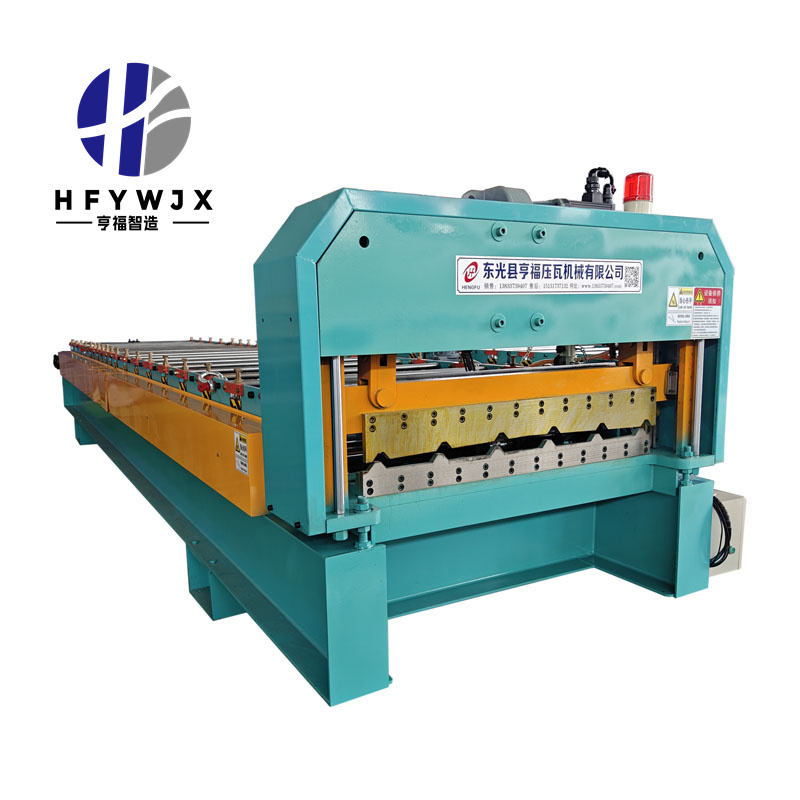
6. How a Cable Tray Machine Works
6.1 Uncoiling and Leveling
Coil is loaded on a robust uncoiler and leveled before processing. For perforated trays, the flat strip then enters the punching station.
6.2 Punching Station
A hydraulic press with a perforation die punches the hole pattern continuously or in indexed strokes. The die determines hole size, shape, and spacing — round, square, or slotted holes. Some lines include separate dies for elongated slots or special fixing points. Punching while flat is far more practical than punching a formed section.
6.3 Forming and Cut-Off
The punched sheet passes through forming stations that fold the side rails, creating the tray profile. The number of stations depends on rail depth and any return flanges. A hydraulic cut-off then shears the tray to length with a profile die. Adjustable-width machines can produce a range of tray widths by repositioning the forming stations, often through quick-change settings.
7. Fittings and Complete System Accessories
Straight tray sections alone do not make a complete cable route. A full system needs a range of fittings, usually fabricated from straight sections or made on dedicated tooling:
- Elbows and bends — change horizontal or vertical direction.
- Tees and crosses — branch or join runs.
- Reducers — transition between tray widths.
- Covers and hold-down clamps — protect and secure cables.
- Splice plates, connectors, and support brackets — join sections and fix to structure.
Offering a complete range of fittings alongside straight sections makes a supplier much more valuable to installers, who want a single source for the whole route.
8. Data Center and Renewable Applications
8.1 Data Centers
Data centers are a major growth driver. They contain dense, organized cable runs over and under racks, with overhead ladder and perforated trays carrying power and network cabling. The scale and repetition of data center fit-outs create large, consistent orders for tray manufacturers, and reliability and clean installation are prioritized over lowest cost.
8.2 Renewable Energy and Industry
Solar farms and wind installations use trays and ladders for field cabling, and battery storage facilities need organized cable routes. Industrial plants, power stations, and infrastructure projects such as tunnels and airports continue to provide steady base demand. These applications favor galvanized, durable trays produced in long, repeatable runs.
9. Installation and Quality Control
9.1 Installation Practice
Trays are mounted on supports or brackets at the spacing used for the load rating, joined with splice plates, and bonded for electrical continuity where required. Cables are laid and tied without exceeding the rated fill, and covers are fitted where specified. Correct support spacing is essential because exceeding it invalidates the load rating and causes excessive sag.
9.2 Quality Checks
- Width, rail depth, and straightness measured on the first piece.
- Hole pattern and spacing checked against the drawing.
- Cut ends square and free of burrs, with galvanizing intact.
- Rails consistent in height so sections join flush.
- Load rating and finish matched to the project specification.
10. FAQ
- What width range do tray machines produce? — Commonly 50–600mm, with some lines covering wider sections. Adjustable machines handle a range rather than a single fixed width.
- Can one machine make several tray sizes? — Yes, adjustable-width lines reposition forming stations for different widths, and quick-change systems reduce the time needed.
- Which material is most common? — Hot-dip galvanized steel for general and outdoor use; stainless steel or aluminum for corrosive environments.
- How fast does a tray line run? — Around 10–18 m/min, with punching slightly reducing effective speed.
- Why are load class and support span linked? — Because capacity is tested over a defined span. A tray carries more over shorter supports, so the rating only applies at the specified spacing.
- Do I need to supply fittings too? — Complete routes require elbows, tees, reducers, and connectors, so offering them strengthens the product package.
- Is demand growing? — Yes, particularly from data center construction and renewable energy, alongside steady industrial and infrastructure demand.
11. Conclusion
Cable tray roll forming machines produce essential cable management components used across virtually every type of modern building and industrial facility. The right machine depends on the tray type — solid bottom, perforated, ladder, or channel — and the width and load range required. Perforated lines with integrated punching are the most versatile and common, while ladder tray production is more complex. Standards such as NEMA VE 1 and IEC 61537 tie load ratings to support spans, so accurate production and correct installation go together. With strong demand from data centers, renewable energy, and ongoing infrastructure work, a well-built cable tray line is a reliable, long-term investment for a sheet metal fabrication business.
References
- NEMA VE 1 — Metal Cable Tray Systems Standard
- IEC 61537 — Cable Tray Systems for Electrical Installations
Writer Robert Taylor
Robert Taylor is a mechanical engineer and technical writer with more than 14 years of hands-on experience in the roll forming and sheet metal fabrication industry. He has commissioned over 120 roll forming lines across 20 countries, covering roofing, structural purlin, cable tray, door frame, and custom profile applications. He holds a Bachelor of Engineering degree in Mechanical Design and Manufacturing, and his published work focuses on practical equipment selection, process optimization, defect troubleshooting, and lifecycle maintenance.